Cast iron breaks in ways steel does not. It cracks cold, it cracks again right beside the first repair, and it does it on the parts nobody wants to throw away: the fence post that matches nothing sold today, the porch column base, the housing on a machine that still earns its keep. So the question comes up fast. Can you MIG weld cast iron, or does the whole piece go in the dumpster? You can, and MIG is the least forgiving of the common ways to do it. Here is what the job takes and where it goes wrong.
Cast iron gets described as steel with extra carbon, and that description is what gets parts broken twice. Gray iron runs roughly 2 to 4 percent carbon, and most of it sits in the metal as graphite flakes rather than dissolved into it. Those flakes are why the material casts cheaply, damps vibration, and snaps when a plow clips it.
They are also why welding it is awkward. Heat a casting fast in one spot and the ring of parent metal around the weld picks up carbon, cools hard and brittle, and shrinks against a cold body that will not move with it. The bead is usually fine. The parent metal an eighth of an inch outside it is where the new crack shows up. Every step below aims at that one problem.
A lot of "cast iron will not weld" stories start with a part that was mild steel, or with white iron that never should have seen an arc. Five minutes of checking saves the repair.
If the file will not bite and the fracture face is bright and crystalline, you are probably looking at white cast iron. That is the one honest no here. White iron has no graphite to absorb stress and it cracks under almost any welding heat. Braze it, replace it, or design around it.
Yes, and this is the unglamorous checklist.
The filler has to be nickel. Solid nickel wire (ERNi-CI) lays a soft, machinable bead that yields as the casting shrinks. Nickel-iron wire (ERNiFe-CI) is stronger and holds up better on ductile iron and anything under load. Plain steel wire gives you a hard, glassy bead that cracks, often before the part is back in service. Nickel is also why MIG on cast iron gets expensive: the wire costs many times what mild steel costs and is soft enough to birdnest in the drive rolls if tension is off.
Clean it to bright metal. Grind the crack into a V you can reach the root of, drill a stop hole just past each end so it cannot keep running, and get paint, rust and oil out of the way. Oil that soaked into the graphite years ago keeps boiling out of the puddle as long as there is heat on it.
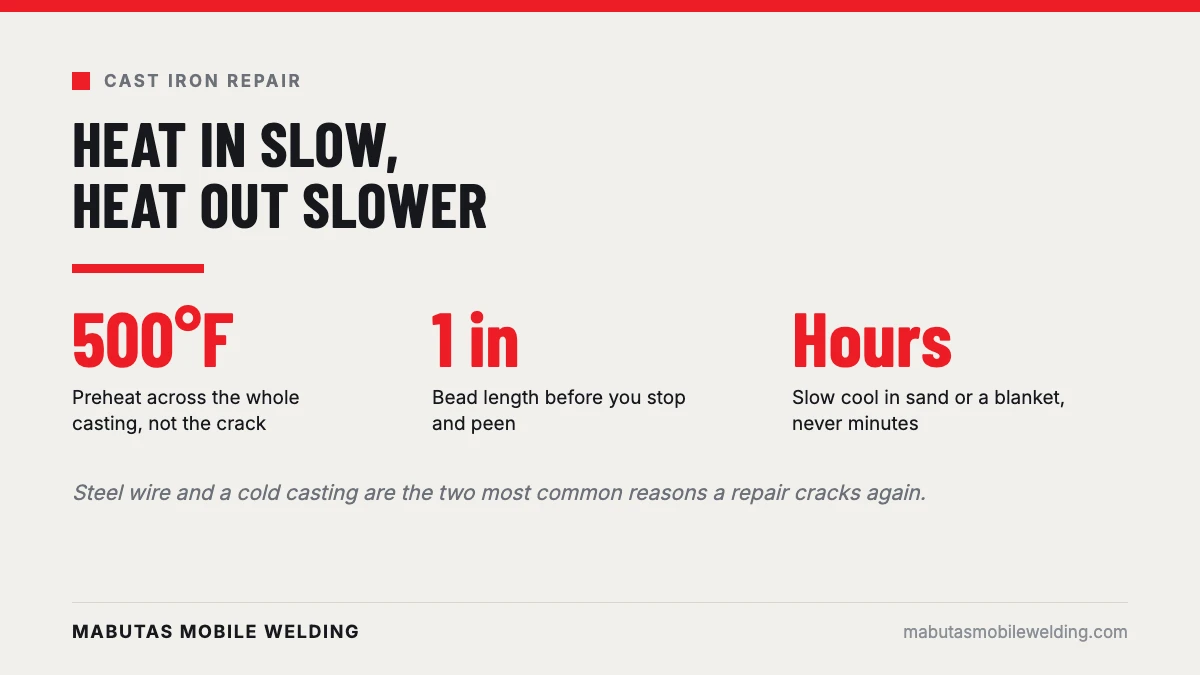
Preheat the casting, not the crack. Around 500°F is the common working figure for gray iron, and the goal is uniform expansion rather than a hot spot. A torch waved at the joint widens the gap between the hot metal and the cold metal holding it.
Run short beads, roughly an inch at a time, then stop. Peen each one with a rounded hammer while it is hot so it stretches back against the shrink. Let the temperature settle between passes.
Cool it slowly. Wrap the part in a welding blanket, bury it in dry sand or lime, or shut it in a box. Slow means hours, not minutes. Setting a hot casting on a cold concrete floor in a January driveway is a quench, and a quench is a crack.
| Approach | Filler on cast iron | Preheat | Cooling | Crack risk | When it is the right call |
|---|---|---|---|---|---|
| MIG (GMAW) | ERNi-CI or ERNiFe-CI nickel wire | Whole casting, around 500°F | Slow, insulated | High if a step is skipped | Longer joints where deposition speed pays, on a part that can be moved somewhere controlled |
| TIG (GTAW) | ERNi-CI or ERNiFe-CI rod | Yes, held through the job | Slow, insulated | Moderate, best heat control | Small, visible or precise work: finials, brackets, thin sections |
| Stick (SMAW) | ENi-CI or ENiFe-CI nickel electrode | Yes, or a low-heat sequence | Slow, insulated | Moderate, most forgiving | Field repairs on dirty, painted or awkward castings |
| Braze welding | Silicon bronze or nickel bronze | Light, below the melting point | Still slow | Lowest, parent metal never melts | Ornamental and non-structural parts, thin walls, tired castings |
Every failure below is avoidable, and every one of them is common.
A repaired casting is a repaired casting. A good nickel weld on gray iron is usually softer than the metal around it, not stronger. On a decorative piece that is fine. On anything carrying load or carrying people, the repair has to be sized and placed with that in mind, or the part gets replaced.
Most cast iron content online is about engine blocks and antique stoves. That is not what the phone rings about here. In Villa Park, Elmhurst, Lombard, Hinsdale and Oak Brook, it looks like this:
The pattern repeats: the part is obsolete, matched to something around it, or bolted into concrete. Replacement is never a five minute swap, which is why welding it carefully is worth the time. When the cracked piece belongs to a fence line, the decision usually widens, and that call is covered in wrought iron fence repair versus replacement.
Stop if the casting carries load or carries people. Stop if it is white iron. Stop if the crack was welded once and came back, because a second failure in the same spot is a stress or design problem, not a filler problem. Stop if the part cannot be preheated where it sits, which rules out anything mounted against siding, wood trim or finished flooring.
On site a mobile rig can grind out the crack, preheat, run nickel electrode, peen the beads and wrap the part for a slow cool. What it cannot do in a driveway is hold a large casting at temperature for hours, or stop a January wind chilling one face while the torch heats the other. Some jobs get cut loose, finished somewhere controlled, then reinstalled. That is a normal answer, not a dodge.
Fence posts, finials, column bases and gate hardware sit inside wrought iron and cast iron fence repair in DuPage County. One-off castings, decorative pieces and parts that need a new section fabricated rather than welded back together fall under custom and decorative metal fabrication. If you cannot tell which one you have, photograph the break. The fracture face answers most of it. If the process side is what you are weighing rather than the material, the companion piece on choosing between TIG, MIG and stick covers how the location decides before preference does.
So, can you MIG weld cast iron? Yes, on the right part, with nickel wire, honest preheat and a slow cool. Everything else on this page is what people skip right before the crack comes back.
Cast iron is not the only metal that punishes a straight in weld. When the part is coated rather than cast, zinc changes the job in a different way: fume you have to control, and a protective layer that has to go back on or the repair becomes the first thing to rust.
Sources: American Welding Society standards, including D11.2 Guide for Welding Iron Castings · ASM International on cast iron metallurgy · OSHA Welding, Cutting and Brazing