Somebody backed into a bollard in a Bensenville lot, a dock guardrail took a hit, or a stair stringer cracked at the weld. Now there is a repair to make on steel that is already coated, and the question on site is always the same. Can you weld galvanized steel, or does the zinc have to come off first? You can weld it. The zinc is the whole problem, and how you handle it decides whether you get a sound joint or a bead full of holes you cannot see, plus a night that feels like the flu.
Hot-dip galvanizing bonds a zinc coating to steel, usually a few thousandths of an inch thick on structural work. It is why a guardrail in an Addison parking lot lasts decades instead of years, and it is why welding it behaves differently from welding bare steel.
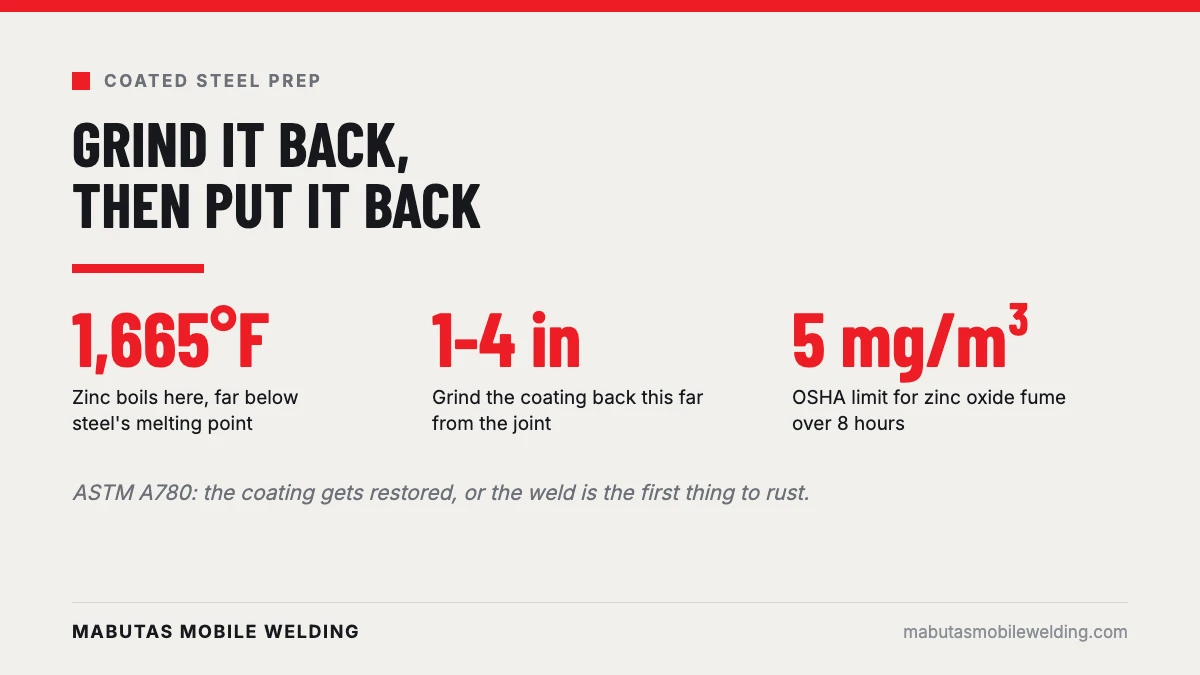
Zinc melts around 787°F and boils around 1,665°F. Steel does not melt until roughly 2,500°F. So the moment the arc strikes, the zinc in and around the joint is already a gas. That vapor has to go somewhere. Some comes up through the molten puddle and freezes in as porosity, some drives into the grain boundaries of the hot metal, and the rest goes into the air at head height, which is where the welder is standing.
None of that makes galvanized steel unweldable. It makes preparation, ventilation and finishing part of the job rather than optional extras.
Breathing zinc oxide fume causes metal fume fever, known on job sites as zinc shakes. Symptoms usually start four to twelve hours after exposure rather than during the work, which is why people fail to connect the two: chills, fever, aching muscles, a metallic taste and nausea, typically clearing within a day or two.
It passes, and that is why it gets shrugged off. Two things worth saying plainly. OSHA sets a permissible exposure limit for zinc oxide fume of 5 mg/m³ averaged over an eight hour shift, and the ACGIH threshold value is lower still, so this is a regulated exposure and not just a rough evening. And welding fume is never only zinc. There is iron oxide, manganese, and whatever primer sat over the galvanizing.
The practical rules are short. Work upwind or with mechanical ventilation. In an enclosed space OSHA requires local exhaust or supplied-air respiratory protection when welding on zinc-bearing base metal. A welding helmet is a face shield, not respiratory protection. And grinding the coating off throws zinc dust, so the particulate respirator goes on before the grinder does.
This is the part that separates a repair that holds from one that only looks like it does.
Take the coating back to bright steel. Not gray, not dull, bright. A flap disc, a wire wheel or a grinding disc all work, and the goal is the same: no zinc left in the weld zone or anywhere the puddle and the heat will reach.
Go further back than feels necessary. The American Galvanizers Association puts the removal zone at roughly one to four inches from the intended weld depending on process and heat input, on both sides of the joint and both faces of the material. Zinc an inch from the arc still vaporizes.
Do not plan to burn it off. Running hot enough to boil the coating away is a real technique and it is the worse option almost every time. It fills the joint with fume, drives zinc into the weld metal, and wrecks the coating far past the area you would have ground anyway.
Then weld it as you would bare steel of the same thickness. Stick and flux core handle field conditions best, and MIG needs shelter from wind the way it always does. The walkthrough on picking between TIG, MIG and stick covers how the site decides that before preference does.
| Situation | Zinc removal | Ventilation needed | Weld defect risk | Coating restoration |
|---|---|---|---|---|
| Grind back to bright steel | Mechanical, 1 to 4 in from the joint, both faces | Fume control for grinding dust plus normal welding ventilation | Low, the joint behaves like bare steel | Required over the weld and the ground area |
| Burn through the coating | None, the arc vaporizes it | High, local exhaust or supplied air | High: porosity, zinc inclusions, cracking | Required over a much larger damaged zone |
| Fabricate first, galvanize after | Not applicable, steel is bare | Standard welding ventilation | Lowest, and the coating covers the welds | None, but hollow sections need vent and drain holes |
| Field repair on installed galvanized steel | Mechanical, as above, in place | Site dependent; enclosed spaces need exhaust or supplied air | Low if prepped, high if rushed | Required, usually zinc-rich paint on site |
The failures are predictable and they show up in a specific order.
Nobody can tell you from a photograph whether a galvanized weld was prepped. The tells are porosity on a cut section and rust appearing at the repair long before it appears anywhere else. If a bid on coated steel does not mention grinding the coating back or restoring it afterward, ask why not.
In this county galvanized is not a specialty material, it is most of the steel that lives outdoors.
Almost all of it shares two traits: it is bolted or set into something that is not moving, and it sits on a property that is open for business. That is where a mobile rig earns its keep, because the alternative is cutting the assembly out and shutting the area down. On railings the code side matters as much as the metal, and the height and gap rules are in the guide to Illinois stair and railing code. For trailer and equipment hardware, the same crack question comes up in whether a cracked trailer frame can be welded.
This is the step most pages leave out, and it is the one the property owner sees a year later.
ASTM A780 is the standard practice for repairing damaged and uncoated areas on hot-dip galvanized steel, and it recognizes three methods: zinc-rich paint, zinc-based solder, and sprayed zinc, also called metallizing. On a live job site zinc-rich paint is almost always the practical choice, because the other two need preparation and equipment a parking lot does not offer.
Two details decide whether it works. The product has to be a genuine zinc-rich coating with a high percentage of zinc dust in the dry film, not a can of aluminum-colored spray labeled to look like one. And the repaired film has to be built at least as thick as the coating around it, which usually means more than one pass with real cure time between them. Remove spatter and slag, take the area back to clean steel, then coat past the edges of the damage. Skip it and a decades-long coating becomes a maintenance item.
Stop if the ventilation is not there. An enclosed dock, a pit, a mechanical room or a tarped-off area is a confined space problem before it is a welding problem, and it needs exhaust or supplied air rather than an open door and optimism.
Stop if the member carries load. Guardrail, stair stringers, platform framing and rack uprights are structural, and a repair on coated steel that was never prepped is a hidden defect in something people lean on. Stop if the same spot has been repaired before, because the second crack is telling you about the design, not the weld.
What a mobile rig can do in a lot or on a dock is grind the coating back, weld with stick or flux core in wind that would ruin a MIG bead, and restore the coating before it leaves. What it cannot do is create ventilation in a sealed space or dip an assembly back in a galvanizing kettle. That is on-site structural welding for DuPage County builders and property managers, and where new galvanized railing or guardrail sections are needed rather than repaired, handrail and guardrail fabrication.
So, can you weld galvanized steel? Yes. Grind the zinc back, control the fume, weld it like bare steel, and put the coating back. Every failure on this page comes from skipping one of those four.
Coating is one material problem, and the metal underneath can be another. If the piece turns out to be a casting rather than rolled steel, welding cast iron is a different job again: nickel wire, a real preheat, and a cool down you cannot rush.
Get a quote on coated steel repair
Sources: American Galvanizers Association on welding galvanized steel · OSHA welding hazards and solutions · OSHA Table Z-1 permissible exposure limits · ASTM A780, repair of damaged hot-dip galvanized coatings